Heat treatment is a technological operation consisting of controlled heating and heat transfer and/or cooling, by which the properties of products can be modified to suit their application. There are certain heat treatments that are used for a particular alloy family – for example for stainless and acid-resistant steels – and there are others that are independent of the material being heat treated. The success of the heat treatment carried out depends on how well the processes taking place within the workpiece are known. It is necessary to know exactly what the temperature distribution within it is, and how that changes over time.
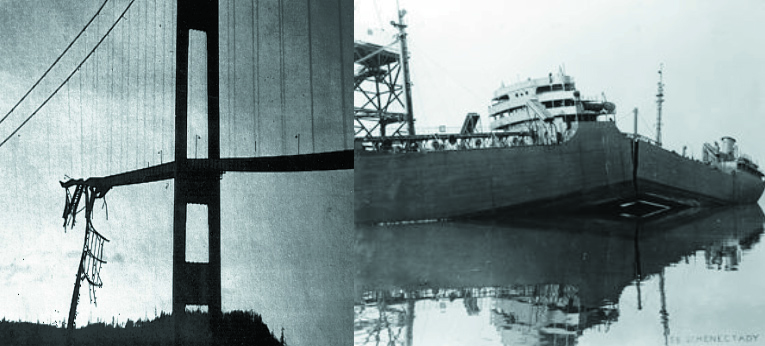
Built into large, cold-operating, dynamically loaded structures, the brittle fracture of materials judged suitable on the basis of conventional tests has led to a series of catastrophes. Embrittlement is a characteristic of body-centred crystalline materials, and so it threatens steel structures, including stainless and acid-resistant steels, as well. The transition temperature and impact energy measurable during the notched-bar impact bending test serve to assess the tendency to embrittlement, and the toughness materials show under normal conditions. The latter can be changed to a significant degree by heat treatment.
01Soft annealing
A heat treatment generally applied to cold-formed semi-finished products. Its purpose is to remove from the material the lattice defects that impede prior and further forming. E.g. a further reduction in the thickness of cold-rolled sheet can be achieved after soft annealing.
02Normalising
It eliminates the irregularities that have formed in the microstructure. It usually consists of austenitising annealing followed by cooling in air; this way a fine pearlitic microstructure forms. The temperature of normalising is determined primarily by the initial carbon content. Normalising is often not the final heat treatment operation, but merely creates the right structure for the next heat treatment.
In contrast, in weldable alloys with a 0.2% carbon content, normalising is not followed by a further heat treatment. In such cases normalising may be justified by the hot-forming temperature having been too high and a coarse structure having formed, or by the workpiece having received a small degree of cold forming, or perhaps by the hot forming having been uneven, or by coarsening formed along the weld seams having to be eliminated. The result of normalising is established by measuring the mechanical properties of the test piece, and not by examining the microstructure.
03Grain-coarsening annealing
During normalising a so-called banded microstructure often forms, which stems from the non-homogeneous distribution of the alloying elements. During machining the periodically arranged ferrite and pearlite bands are very unfavourable. The microstructure is therefore coarsened.
04Recrystallisation heat treatment
When cold-formed products are heated, undeformed grains develop at the expense of the deformed grains. (Cold forming of steels deforms the grains, and this creates work hardening. The work hardness can be eliminated by annealing. Heated to approximately 400–650 ºC, new, undeformed grains come into being at the expense of the deformed grains. The resulting grain size determines the properties. (The grain size depends on the degree of forming and on the temperature and time of heating.)
The properties of annealed products are determined by the grain size that has formed. And this depends on the degree of cold forming and on the temperature and duration of heating. The recrystallisation diagram gives guidance on the expected result. In general a fine-grained condition should be aimed for, but with transformer sheet, for example, the magnetic properties are the more favourable the coarser the grains. In many cases partial annealing must be applied, that is, recrystallisation must only be partially achieved. This is how, for example, semi-hard wires can be produced from wire drawn to spring hardness. To check the success of annealing, a hardness test or a tensile test can be used, supplemented with forming-technology tests.
05Stabilising heat treatment
During such a heat treatment – as its name suggests – the aim is to stabilise the structure. For example, during the stabilising annealing of weathering steels and of certain acid-resistant steels, copper precipitates in the alloy. During use the surface rusts, the iron transforms into a loosely structured oxide, so close to the surface the copper is enriched, thereby preventing further oxidation (rusting).
For such a protective layer to form, the steel must first rust, which is why such products must not be painted.
06Stress-relief heat treatment
During the various technologies, harmful residual stresses can arise in the products. These are harmful from two points of view. On the one hand they are added to the stresses caused by the operating load, thereby reducing the load capacity and the service life; on the other hand, over a long period, the relaxation of the residual stresses can result in dimensional change or warping of the part. It is therefore advisable to relax the residual stresses with stress-relieving heat treatments.
The most common tasks:
- Relaxing the residual stresses of castings before machining, so that the warping occurs before machining.
- Stress relief after rough machining and before final machining, so that the warping takes place before the final dimension is formed.
- Relaxation of cold-formed products, or of slender products after cold-forming straightening, so that the relaxation of the forming stresses does not occur during storage or use, causing warping.
- Stress relief of hardened parts and tools by relaxing the macroscopic and microscopic residual stresses, in order to reduce brittleness and increase service life.
- The breakdown of the residual stresses is the faster and the more complete the higher the temperature at which the heating takes place. In order to prevent the stresses from arising again, the heating must be followed by very slow cooling (50-100°C/h).
- The general rule when choosing the relaxation temperature is that the highest temperature must be chosen at which no processes harmful from other points of view yet take place. Accordingly, for example:
- the softening of cold-formed products must not exceed what is prescribed,
- the reduction in hardness of hardened or quenched-and-tempered products must not exceed what is prescribed, etc.
On this basis, even 650-680 ºC can be used for the stress relief of castings and welded structures, but in the case of quenched-and-tempered products one must not heat above the tempering temperature. Hardened and cold-formed products already begin to soften above 250 ºC, so this can roughly be regarded as the limit temperature.
07Quenching and tempering
Quenching and tempering is a compound heat treatment, consisting of hardening and tempering. Its purpose is to produce a fine-grained, so-called spheroidised (quenched-and-tempered) microstructure. This comes about through the decomposition of the hardened microstructure during tempering. The higher the tempering temperature and the longer the holding time, the more complete the decomposition process. As a result, increasing the tempering temperature* reduces the hardness and the strength, while in contrast the impact energy and the formability increase.
Finally, by increasing the temperature, the complete elimination of the effect of hardening can be achieved and the annealed condition is restored. For a given steel grade (chemical composition) the parameters of the quench-and-temper heat treatment must be determined so that the value of the prescribed strength and impact energy to be met is also appropriate. A complex optimisation task therefore has to be solved.
08Case-hardening heat treatments
The purpose of case-hardening heat treatments is generally to increase the surface wear resistance of parts, in such a way that the core of the parts is tough, that is, resistant to fracture. This can be achieved on two different principles.
The two principles of case hardening
- By a heat treatment in which the chemical composition within the piece does not change, but the heat-treatment condition, that is, the structure, does. In such a case the toughness of the core is provided by the quenched-and-tempered condition, and the hardened structure of the case can be created by locally austenitising and hardening the case of the quenched-and-tempered piece. This can be achieved by flame hardening, induction hardening, electron-beam hardening**, laser hardening, etc. The most widespread is case hardening by induction hardening.
- The other way of case hardening is thermochemical treatment. In this case the surface of the piece is enriched by diffusion with some element, so the core and the case have a different chemical composition.
09Carburising
The essence of carburising is that, by diffusing carbon into the case of low-carbon steels, the carbon content of the case can be increased to a level characteristic of quenchable and tempering steels, or even of tool steels. If the whole piece is subsequently austenitised and then hardened, the core does not harden because of the low carbon content and remains soft and tough, while the case will have a wear resistance corresponding to the carbon content.
*Quenching and tempering is a compound heat treatment, consisting of hardening and tempering. Its purpose is to produce a fine-grained, so-called spheroidised microstructure. This comes about through the decomposition of the hardened microstructure during tempering. The higher the tempering temperature and the longer the holding time, the more complete the decomposition process. As a result, increasing the tempering temperature reduces the hardness and the strength, while in contrast the impact energy and the formability increase.
**The beam directed at the workpiece consists of accelerated electrons. The kinetic energy of the electron beam is converted into heat energy on impact, whereby the surface layer melts and evaporates before the heat generated reaches the material by conduction. It can only be used in a vacuum.
Source:
Teaching aid by Dr. Kisfaludy Antal and Borossay Béla
Dr. Gácsi Zoltán and Dr. Mertinger Valéria: Fémtan
Leave a Reply